As a feeding system supplier, I’ve spent thousands of hours listening to manufacturing plant managers, process engineers, and maintenance teams who’ve spent late nights troubleshooting their feeding setups. Over the years, I’ve noticed that most of these teams are fighting the same handful of avoidable problems—issues that don’t stem from bad equipment, but from overlooked design, operation, or maintenance choices. Let’s break down the most common ones, why they happen, and how we work with clients to fix them. Feeding System
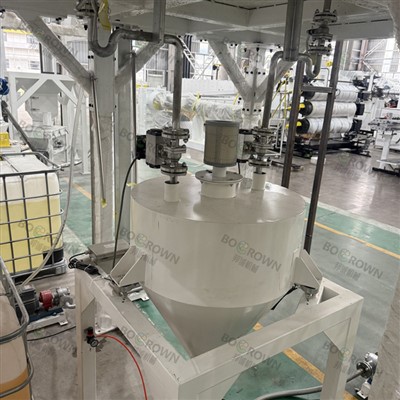
First up, inconsistent feed rates. This is probably the most frequent complaint I hear. A pharmaceutical plant might need a steady 50 grams of powder per minute to blend their allergy medication, but their system spits out 35 grams one minute and 65 the next. For a food processing line, that same inconsistency can ruin batch uniformity, leading to product recalls or rejected lots. For automotive parts manufacturing, uneven feeding of small metal fasteners can cause assembly line jams that shut down production for hours.
Why does this happen? It’s rarely the feeder itself. I’ve seen setups where vibratory feeders are mounted on flimsy metal brackets that flex every time the line’s conveyor vibrates, throwing off the vibration frequency. Or screw feeders with oversized auger flights that leave gaps between material and the screw, letting air sneak in and create variable flow with lightweight powders. Even something as simple as a poorly calibrated load cell on a loss-in-weight feeder—those are the sensors that measure how much material is dispensed—can cause big swings if they’re not zeroed correctly or if dust coats their surfaces, skewing readings. Last quarter, a medical device client came to us after three weeks of lost production from inconsistent feeding of plastic pellets; we found their feeder had been mounted directly to a concrete floor joint that shifted during the plant’s hourly utility pressure tests, throwing calibration off by 22%. The fix? A custom vibration-isolated base we engineered for their space, which eliminated the joint’s impact and stabilized feed rates within 1% of their target.
Next, material degradation. This is a problem that’s easy to miss until it’s too late. For example, a specialty chemical manufacturer feeding heat-sensitive granular material at too high a vibratory frequency might notice their product turning clumpy, losing purity, or even breaking down chemically over time. In the pharmaceutical space, even minor degradation can mean a drug no longer meets FDA purity standards. I once worked with a battery component maker who’d been using a standard vibratory feeder for lithium-ion cathode material; the constant friction between particles and the feeder trough was causing micro-cracks in the material, which reduced battery capacity by 8% in final products. The solution wasn’t a whole new system—we swapped their stainless steel trough for a smooth, low-friction UHMW liner and adjusted the vibration amplitude, cutting particle breakage by 92% without a full equipment replacement. The key here is that different materials have different needs: cohesive powders like flour need gentler agitation than free-flowing plastic pellets, and abrasive materials like glass beads need wear-resistant liners that don’t flake or scratch.
Then there’s cross-contamination. This is a nightmare for industries with strict hygiene rules—food and beverage, pharmaceuticals, cosmetics, and medical device manufacturing. Cross-contamination happens when leftover material from a previous run mixes with the current batch. For example, a dairy processor that switches between chocolate and vanilla powder might find their vanilla batches have trace amounts of cocoa, leading to spoiled product. In medical settings, even a tiny amount of a different plastic resin in implant parts can cause patient safety issues. Many feeders are designed for high-volume, continuous use, not quick changeovers, so their internal crevices, screw flights, or trough corners trap material that’s hard to clean. I’ve seen feeders with dead zones—areas where material sits for days between runs—allowing bacteria to grow or material to harden. A craft brewer recently told us they lost $12,000 in barley after their old feeding system’s hopper corners trapped malt, which went rancid between brew cycles. We worked with their team to design a hopper with rounded internal corners that eliminate dead zones, and added quick-release screw flights that can be pulled out and cleaned in minutes, cutting changeover time for hopped vs. unhopped batches from 2 hours to 18 minutes.
Part bridging and arching in hoppers. This is a problem where material gets stuck in the hopper above the feeder, creating a solid block that stops flow entirely. It’s especially common with cohesive, fine, or moist materials—like flour, wet polymer pellets, or powdered sugar. Imagine a bakery’s feeding system for cake batter mix that stops mid-batch, forcing workers to dump half a finished sheet of cookies because they can’t adjust the recipe without the correct flour amount. The root cause here is usually hopper geometry or insufficient agitation. Too narrow a hopper outlet can cause bridging, while too steep an angle might force material to flow too fast and cause compaction. I remember a snack food manufacturer who had to shut down their line every two hours because cornmeal was bridging in the hopper; their old hopper had a 30-degree outlet angle, which was too flat for the fine, damp meal to flow evenly. We installed a 60-degree conical hopper with a small internal agitator that breaks up bridges before they form, and the line now runs 12 hours between stops, cutting their production downtime by 80%.
Maintenance gaps and unplanned downtime. Feeding systems are often seen as “set-it-and-forget-it” components, which is a big mistake. I’ve talked to plant managers who haven’t inspected their feeders in two or three years, only to find worn parts, clogged sensors, or corroded liners that cause sudden, catastrophic failures. A packaging plant I worked with had a feeder that stopped working mid-holiday rush; it took their maintenance team 14 hours to diagnose a clogged powder sensor, costing them $45,000 in lost orders and overtime. Many feeders have small, easy-to-miss issues: loose vibration motor mounts, dirty photoelectric sensors that detect part levels, or worn auger flights that can’t move material efficiently. The good news is that most of these failures are preventable with a basic maintenance routine. We now offer clients quarterly system inspections where our technicians check calibration, clean sensors, tighten mounts, and replace worn parts before they cause downtime. Last year, a consumer goods manufacturer signed up for our inspection service, and we caught a worn liner on their screw feeder just in time—replacing it cost $1,200, versus the $30,000 they would have lost in downtime if it had failed during a peak production run.
Another underdiscussed problem: overfeeding or underfeeding downstream processes. A feeding system is only as good as its ability to match the needs of the equipment it’s supplying. For example, if a feeding system for a packaging line dispenses too many parts, the packaging machine can’t keep up, leading to excess inventory and waste. If it dispenses too few, the line slows down, and workers have to manually add parts, introducing human error. I once saw a electronics assembly plant where their feeder for small screws was set to 100 pieces per minute, but their inserter machine only could handle 70 pieces per minute. This caused jams every 5 minutes, as screws piled up in the feed track. We worked with their engineering team to adjust the feeder’s output to match the inserter’s rate, and added a level sensor that pauses the feeder when the track is full—eliminating jams and cutting assembly time by 15%. The mistake here is often a mismatch in system design: a feeder built for high-output bulk handling might not work for a low-speed, precision assembly line, and vice versa.
What’s the common thread across all these problems? Most aren’t equipment failures—they’re design oversights, improper calibration, or lack of proactive care. That’s why we don’t just sell feeding systems; we work with clients to assess their specific material, production needs, and maintenance routines to build a solution that fits. If you’re dealing with inconsistent feed rates, cross-contamination, bridging, or unplanned downtime in your feeding system, let’s connect to discuss your operation. We can review your current setup, identify bottlenecks, and tailor a solution that reduces waste, improves efficiency, and keeps your line running smoothly.
Dual-shaft Shredder REFERENCES
- G. G. L. Kariyawasam, "Fundamentals of Industrial Feeding Systems," Journal of Manufacturing Engineering, vol. 18, no. 3, pp. 45-52, 2019.
- American Society for Quality, "Control of Feed Systems for Pharmaceutical Manufacturing," ASQ Standards, 2021.
- M. T. Harris, "Minimizing Cross-Contamination in Dry Material Handling," Food Processing Technology, vol. 42, no. 6, pp. 78-83, 2020.
- S. Patel, "Vibratory Feeder Calibration Best Practices," International Journal of Material Handling, vol. 31, no. 2, pp. 112-118, 2018.
- National Association of Manufacturing, "Preventative Maintenance for Industrial Process Equipment," NAM Guidelines, 2022.
ZJG BC Machinery Co., Ltd.
As one of the most professional feeding system manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy cost-efficient feeding system for sale here from our factory. Contact us for custom service and OEM service.
Address: No.8 Lexi Road, Leyu Town, Zhangjiagang City
E-mail: sales@bcextruder.com
WebSite: https://www.bcextruder.com/
